
Robotic Flame Beveling: Locate the Edge First
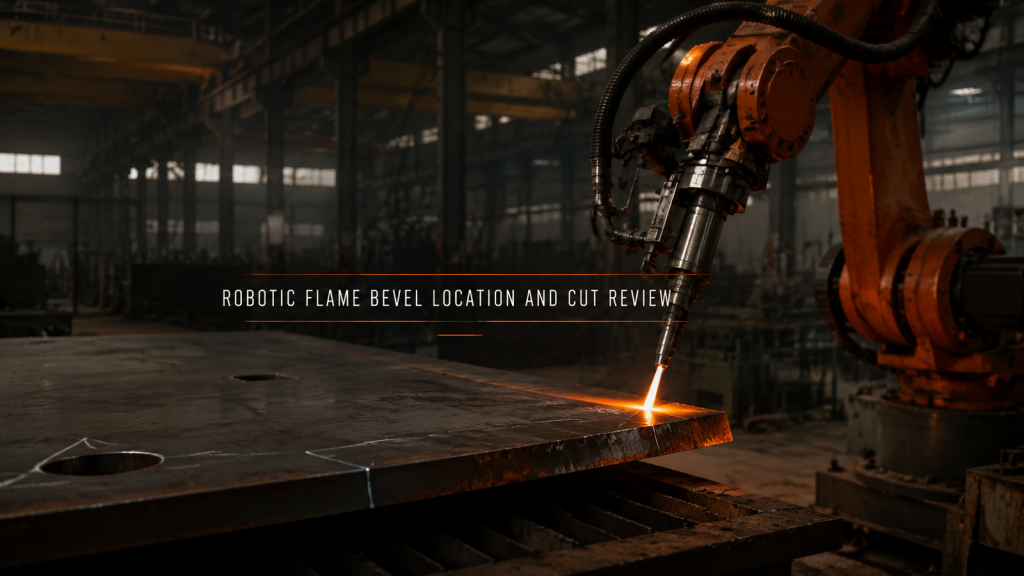
Robotic flame beveling needs a stable plate datum, measured edge location, continuous tool posture and cut-edge acceptance evidence.
Battery Tray Robotic Welding: Datum Before Path
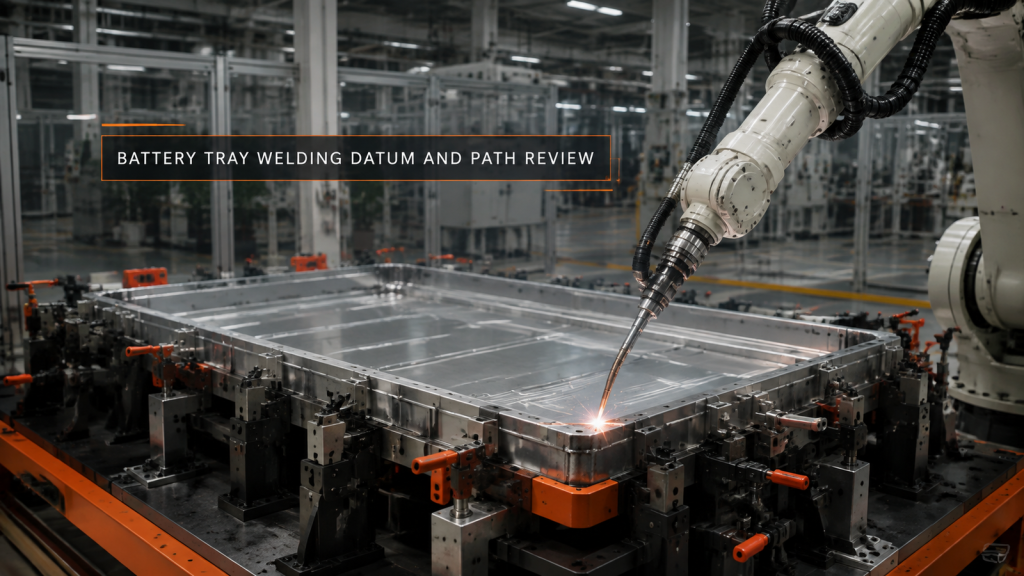
Battery tray robotic welding starts with a stable fixture datum, zoned seams, full-path torch clearance and a measured distortion plan.
Cookware Polishing: Stabilise the Part Pose
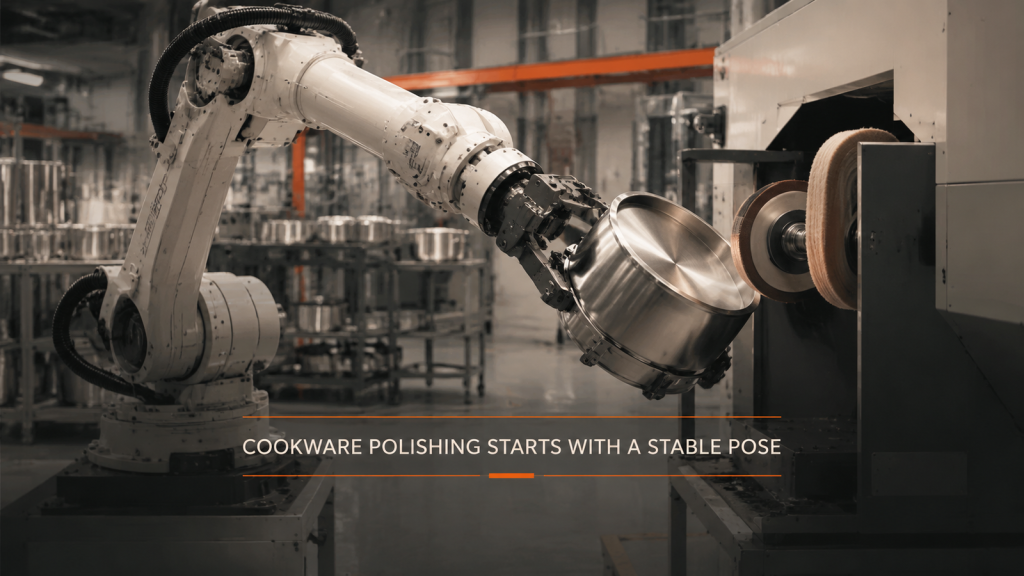
Cookware polishing automation starts with a stable grip datum, complete approach, controlled surface angle and clear retreat before pace is estimated.
Rebar Processing Automation: Locate Before Transfer
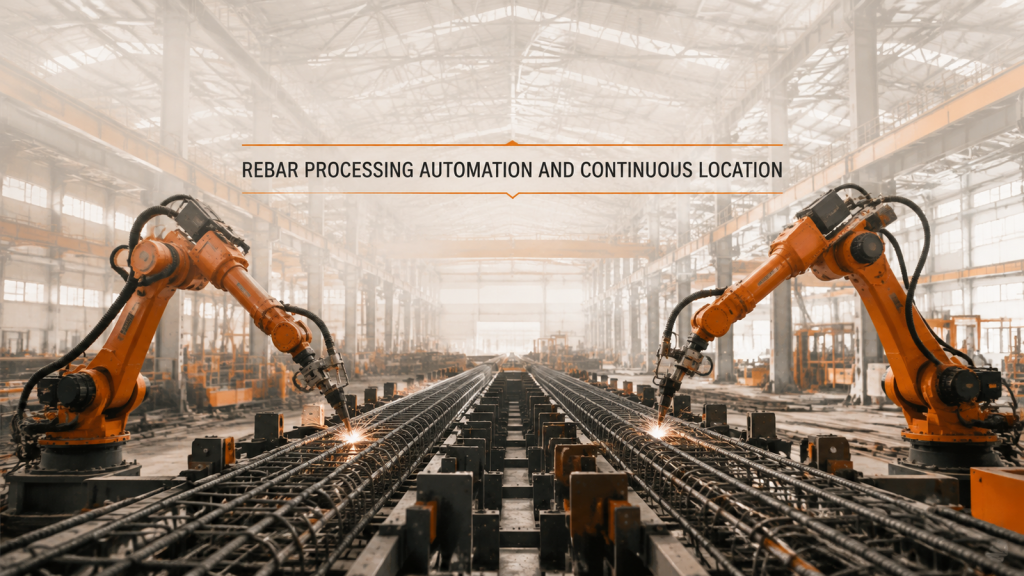
Rebar processing automation needs a continuous datum along a long assembly before transport and two-robot coverage can repeat reliably.
Robotic Die-Casting Tending: Prove the Path First
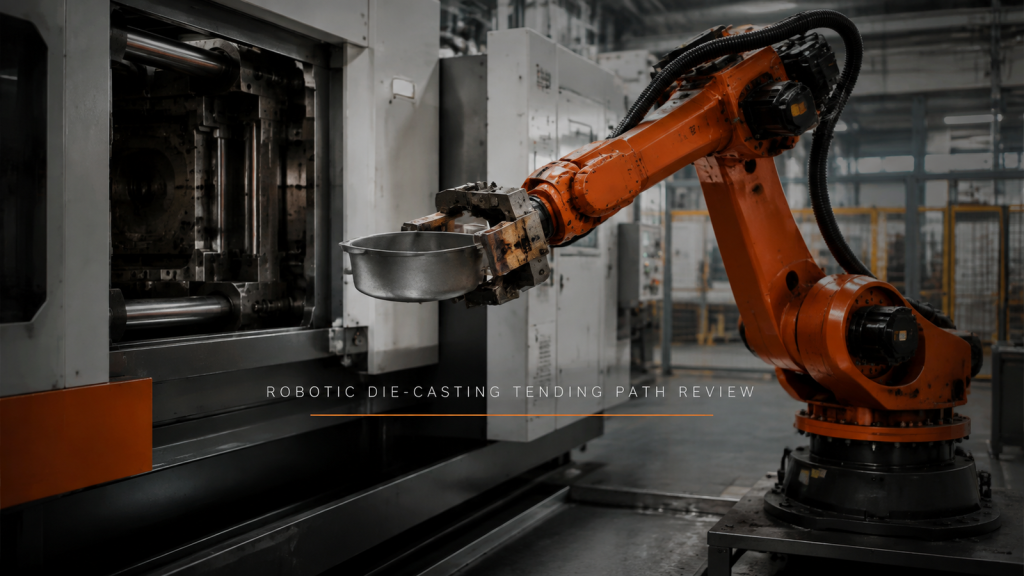
Robotic die-casting tending begins with a verified approach, grip, clear exit and drop route before cycle-time assumptions are made.
Reach Is a Set of Postures, Not a Distance
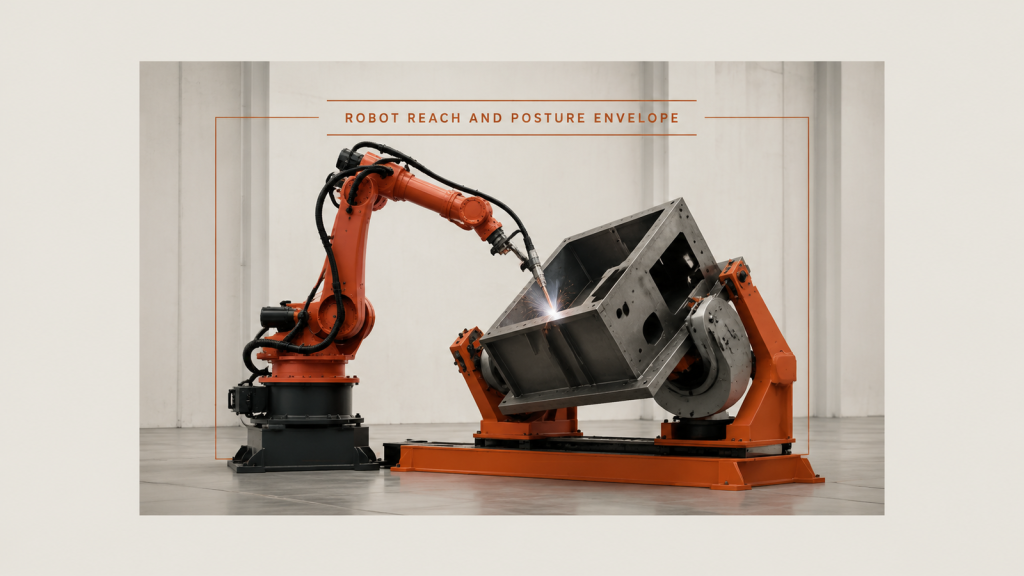
Robot reach and posture envelope: access is decided by posture, which changes along one seam and starts again at the next, not by a single distance.
After Cold Bending, the Part Has to Be Located Again
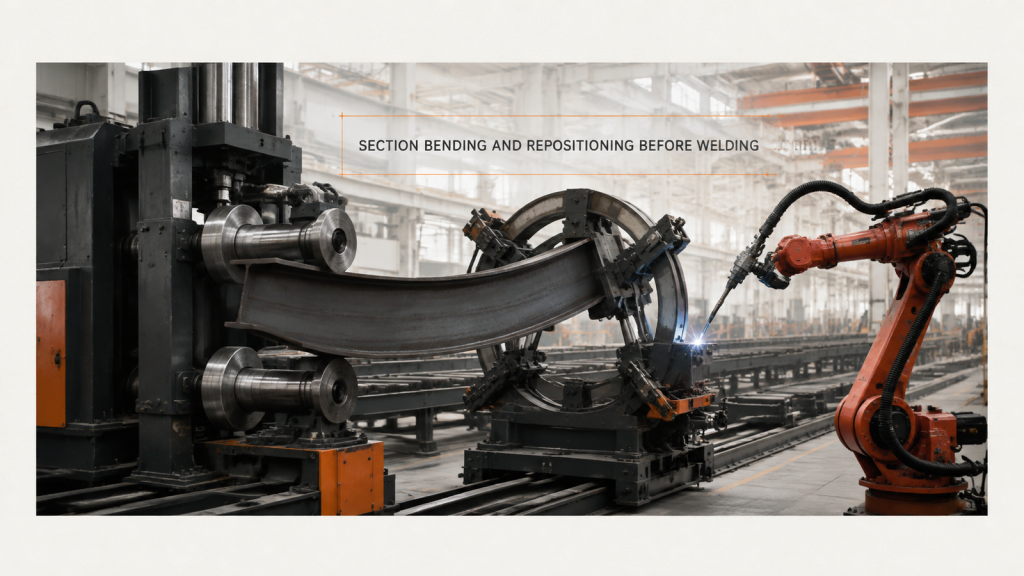
Cold bending curves the face a section was located from, so section bending and repositioning means clamping the arch again before any seam is welded.
Tank Structures: Turn the Fillet or Move the Torch
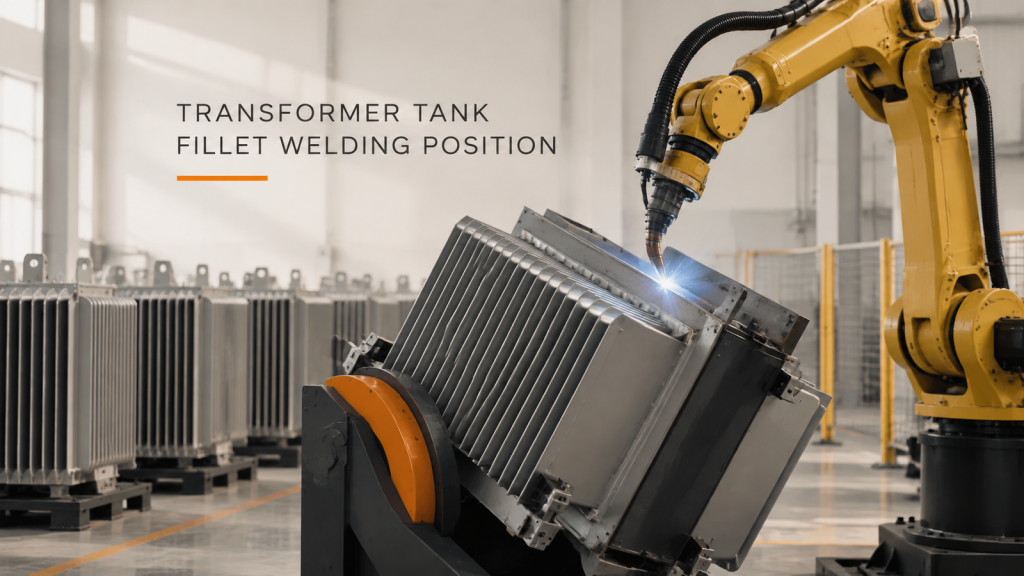
Tank assemblies carry two seam families: long seams are a heat-input problem, stiffener fillets an access problem. They are not solved alike.
Rail, Positioner, or Both: Large Structure Welding
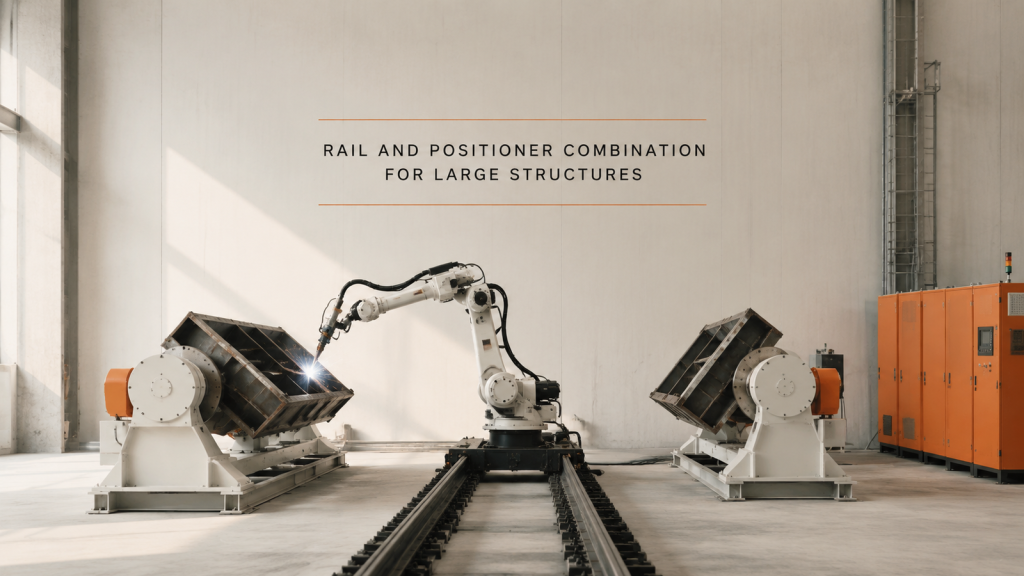
A rail answers reach and a positioner answers attitude. Deciding which a large structure needs starts with the seam list, not with the equipment catalogue.
Intersecting Pipe Joints: Fit-Up Decides the Weld
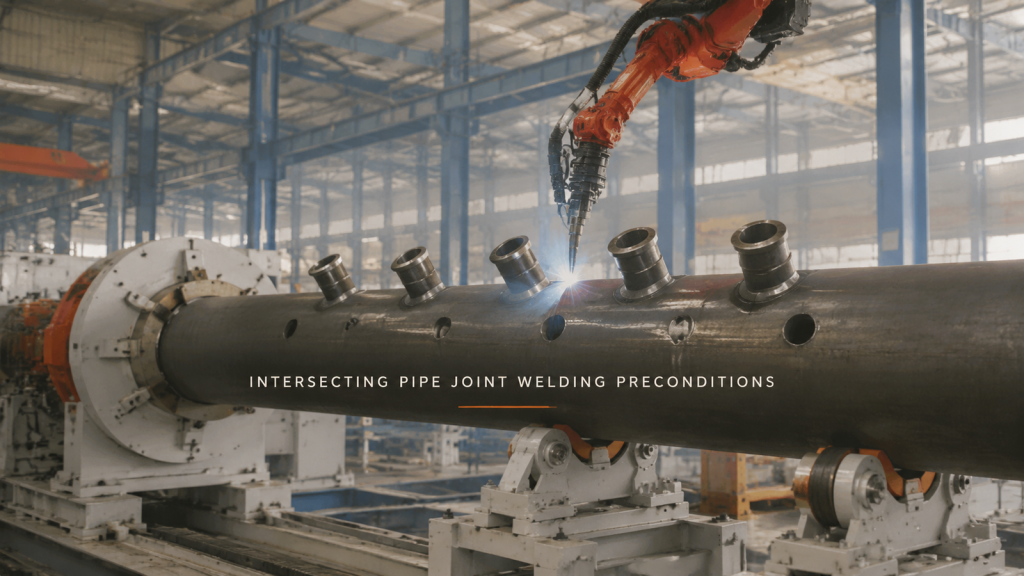
On branch-to-header joints the limiting factor is rarely reach. Hole position, bevel and assembly gap decide whether the seam can be welded in one pass.
Teach-Free Welding: Where It Actually Holds Up
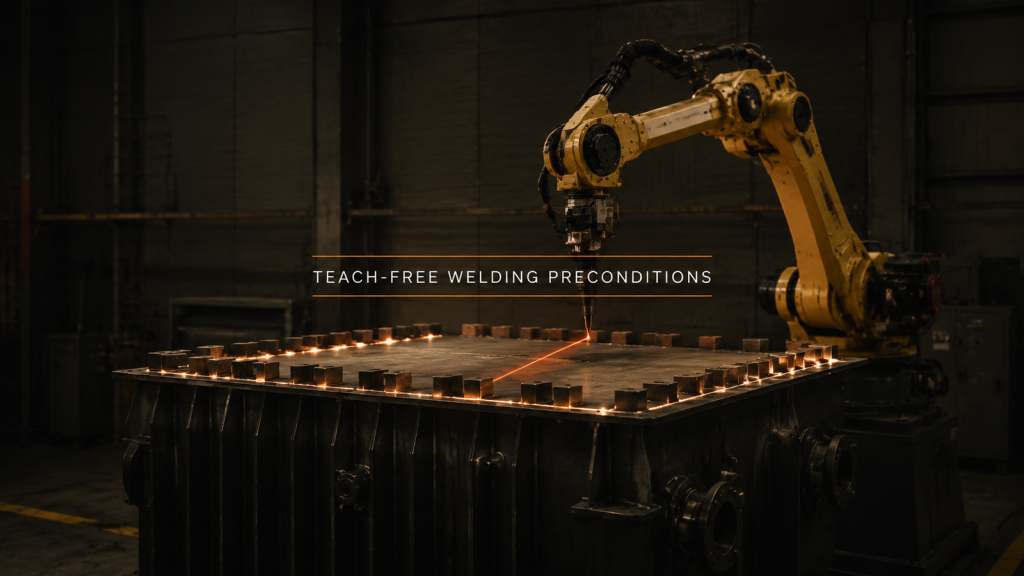
Teach-free welding removes the teaching, not the locating. It holds up where the seam is regular and the variation is something the scan can see.
Welding Fume and Arc Light: The Part Decides
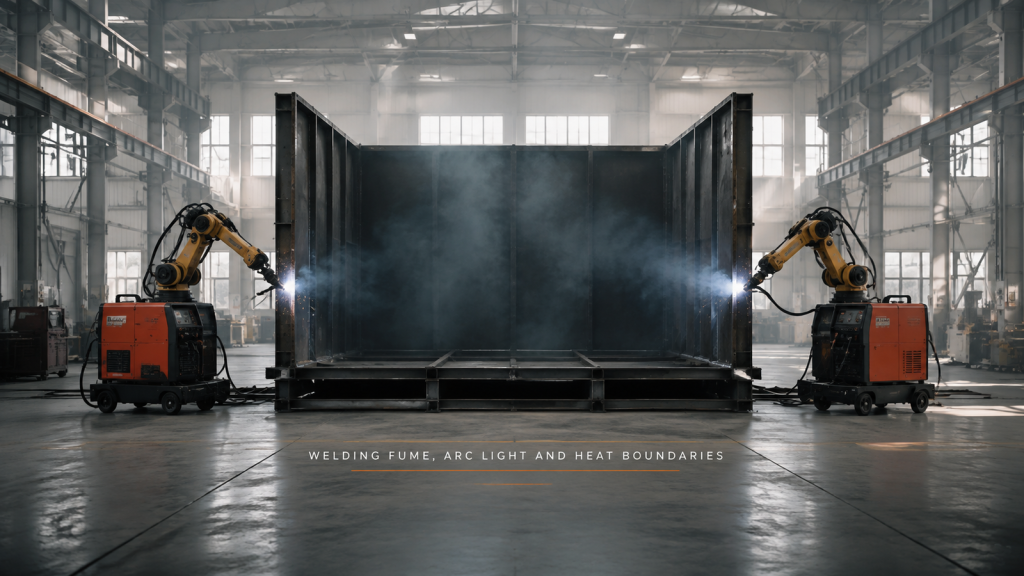
Whether fume can leave a weld is set by how enclosed the part is, and shielding follows where people walk, not the machine footprint.