
On-Site Robotic Welding: Floor, Blocking, Cable
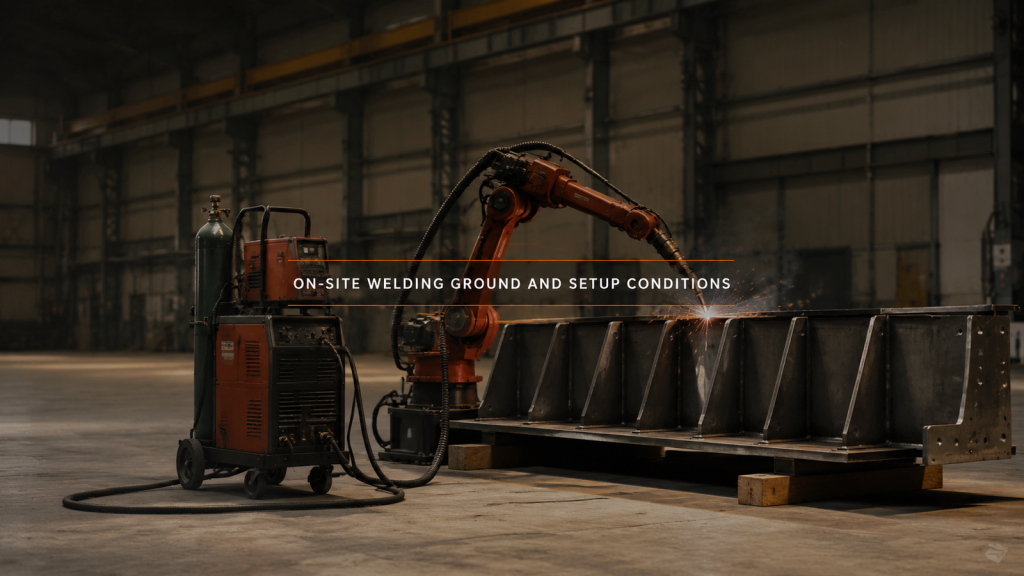
When the part cannot be lifted, the welding unit drives to it, and the floor, the blocking and the trailing cable become the setup.
Dedicated Welding Machine or Robot: Is the Product Settled?
Dedicated welding machine versus robot selection turns on how settled the product is: what each arrangement buys, and what change costs.
Fan Manufacturing Automation Retrofit: Constraints First
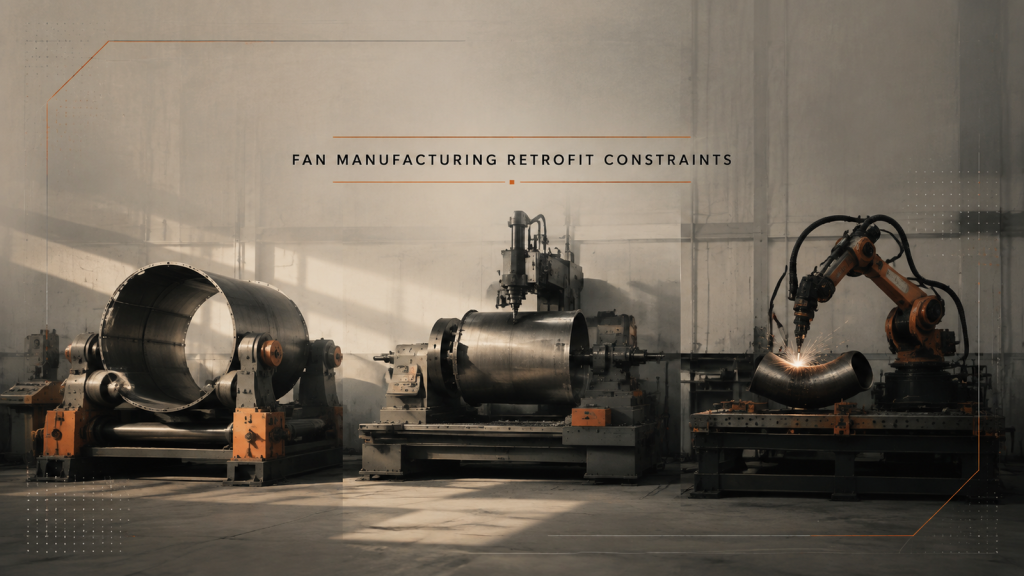
A fan manufacturing automation retrofit faces a chain, not a station. List the constraints before choosing any robot.
Prefabrication Automation: Cost the Handover
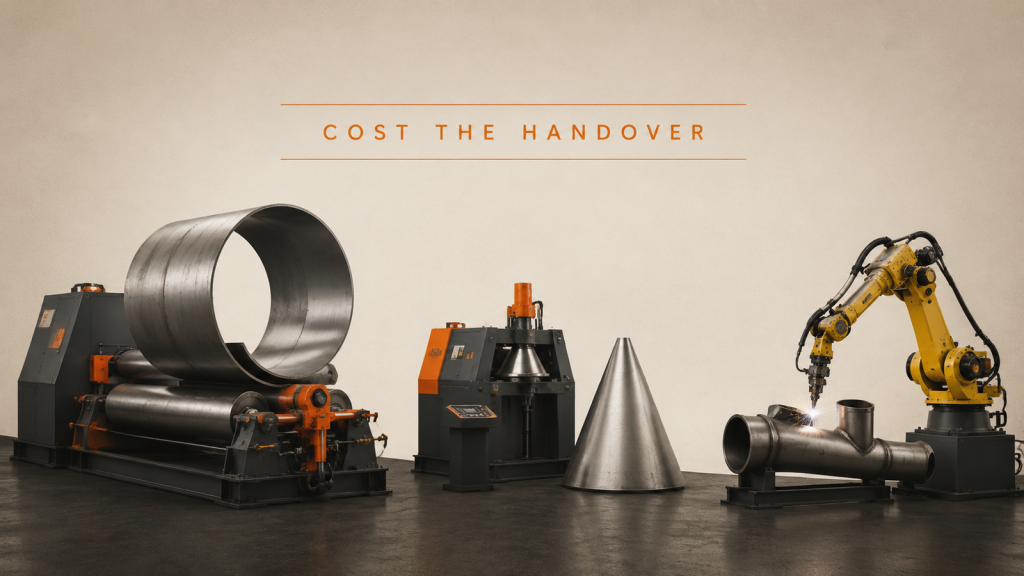
In prefabrication automation, rolling, forming and welding each automate well on their own. What governs output is the handover between them.
Robotic Head Cutting: Path, Attitude and Edge
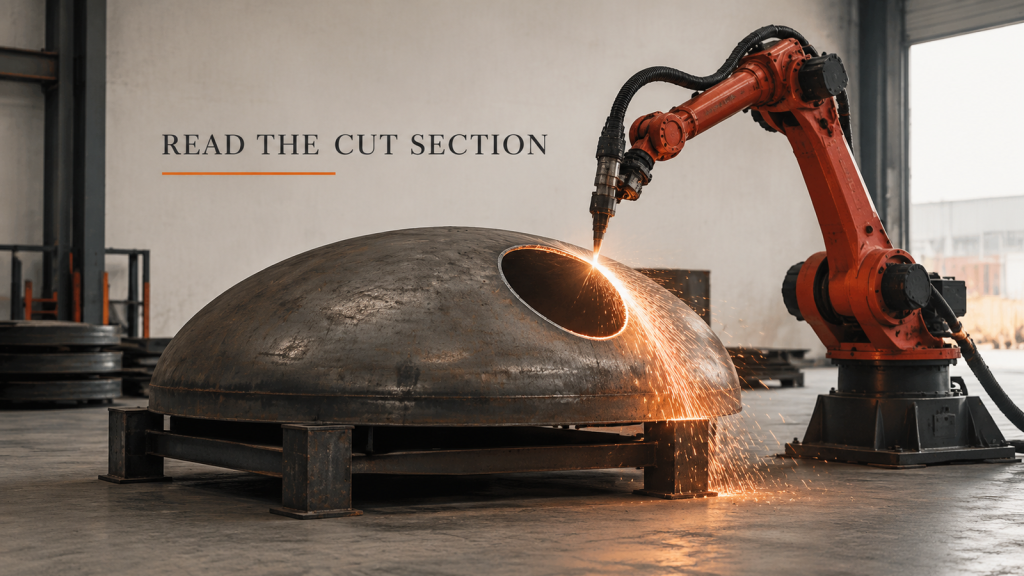
Robotic head cutting puts a closed path on a curved surface. Plan the path and the torch attitude together, then judge the cut edge.
SCARA Robot or Six-Axis: Let the Motion Choose
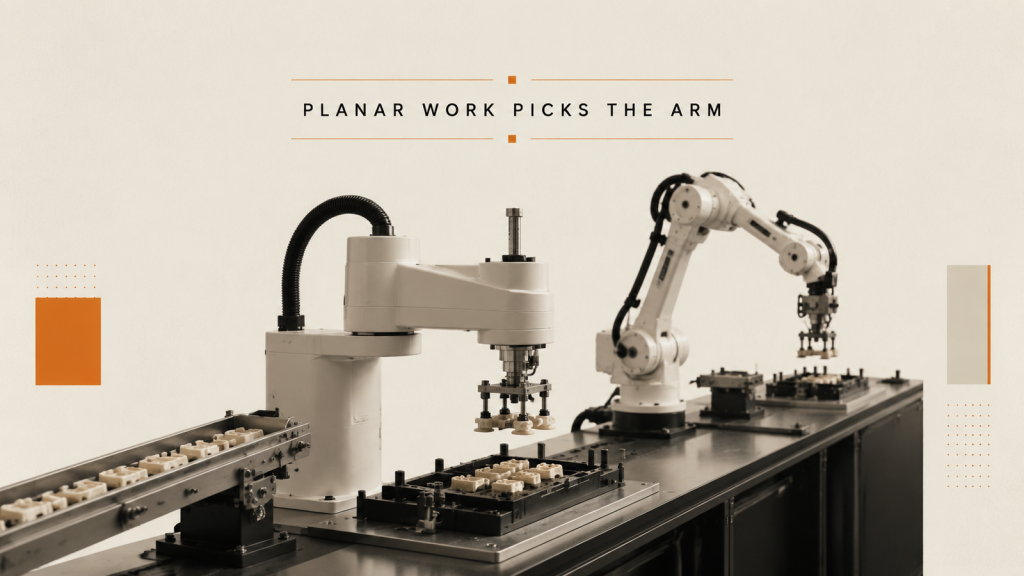
Choosing a SCARA robot or a six-axis arm for small part assembly starts with the motion of each step, not with the axis count in a catalogue.
Robot Payload: Why the Gripper Belongs in It
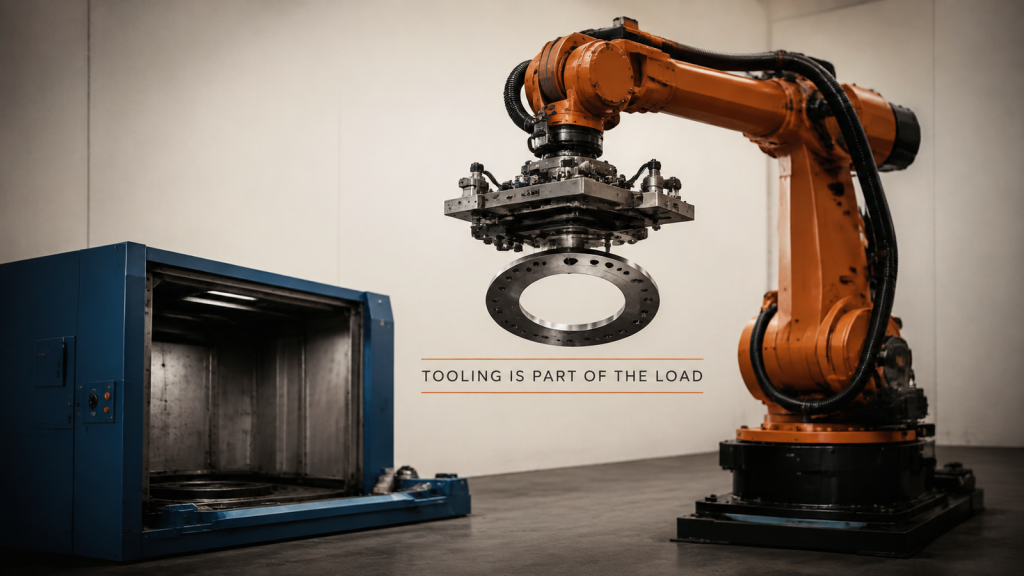
Robot payload has to cover the tooling and the part together, at the real distance between the wrist flange and the centre of mass.
Weld Acceptance: Appearance Is Visible, Penetration Is Not
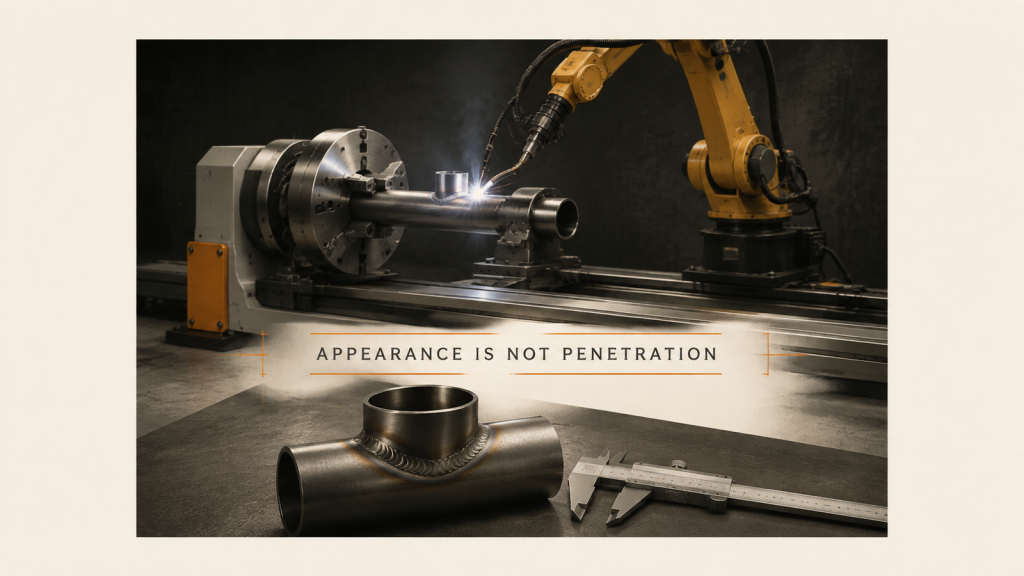
Weld acceptance fails when appearance and penetration are written as one clause. Separate the line-side check from the procedure test.
Cobot Reach: Both the Pick and the Assembly Point
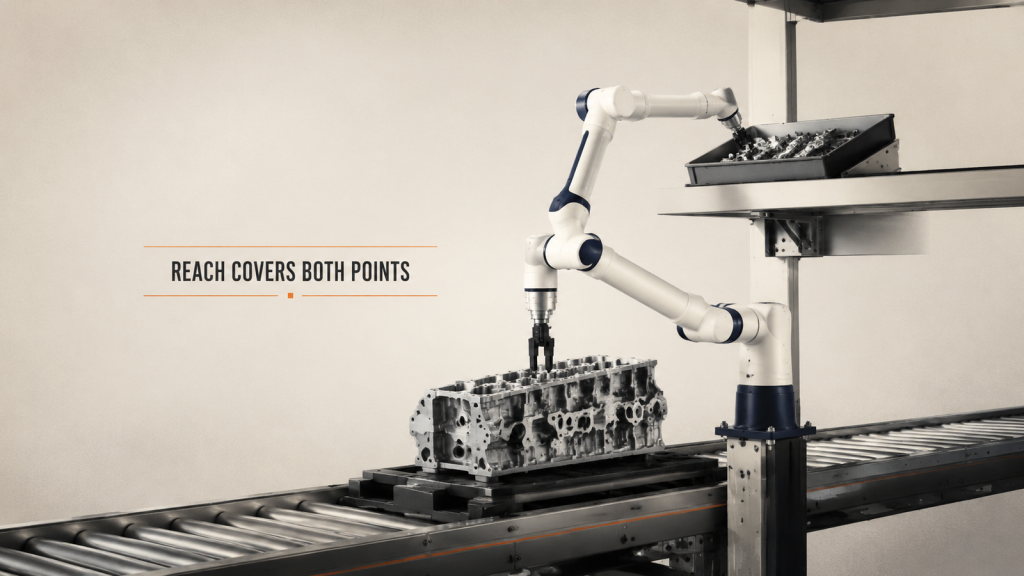
Cobot reach is not one straight-line distance. Every working point, tool length, posture margin and people clearance belong in the same check.
Mobile Welding: Plan Work Positions for Large Parts
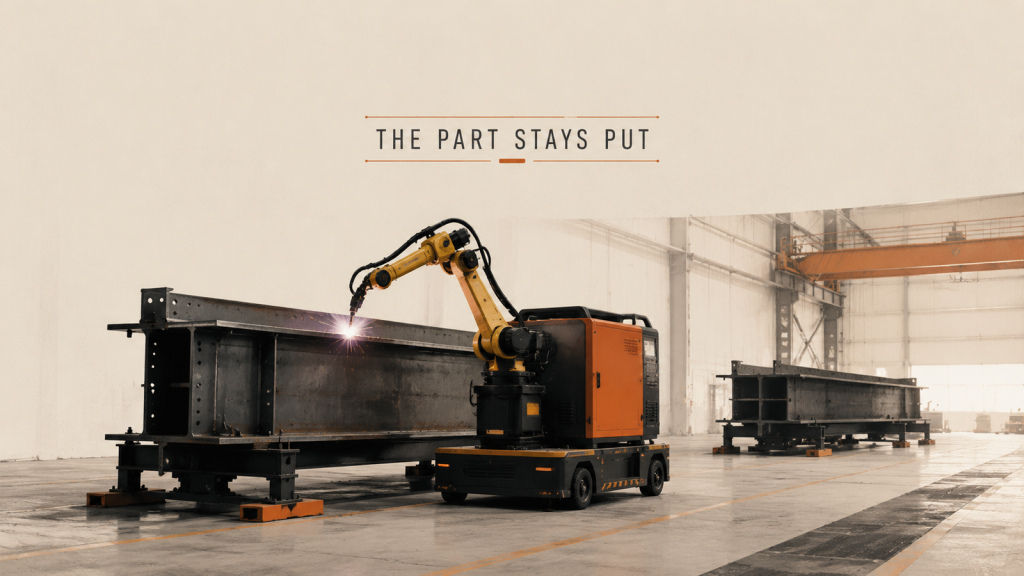
When a part is too large to lift, mobile welding moves the equipment instead. Parking position and datum recovery become the planning unit.
Machine Tending: One Robot Serving Several Machines
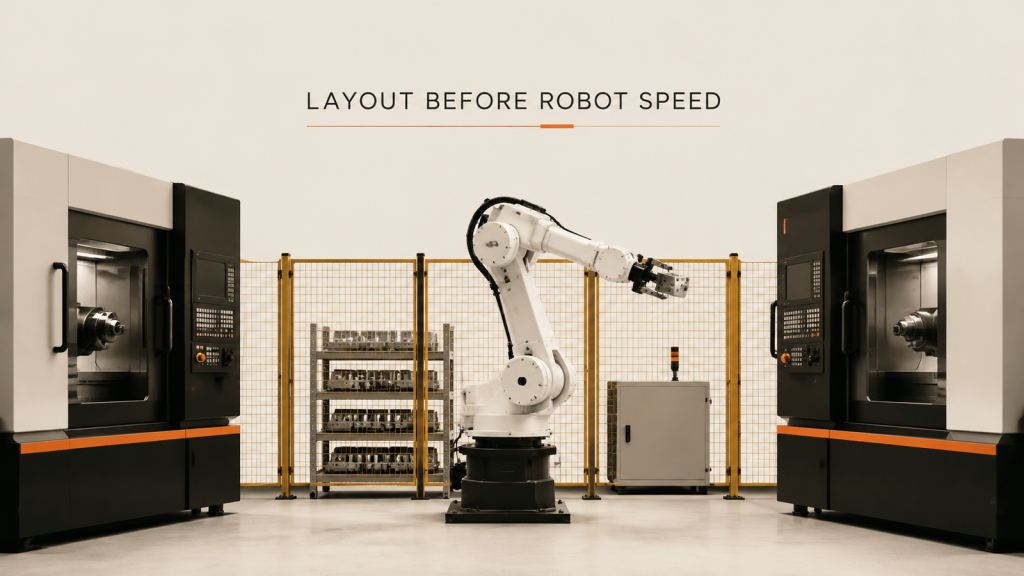
In machine tending with one robot and several machines, reach, waiting and fenced access decide the case long before arm speed does.
Thin-Sheet Welding: Distortion Starts at Clamping
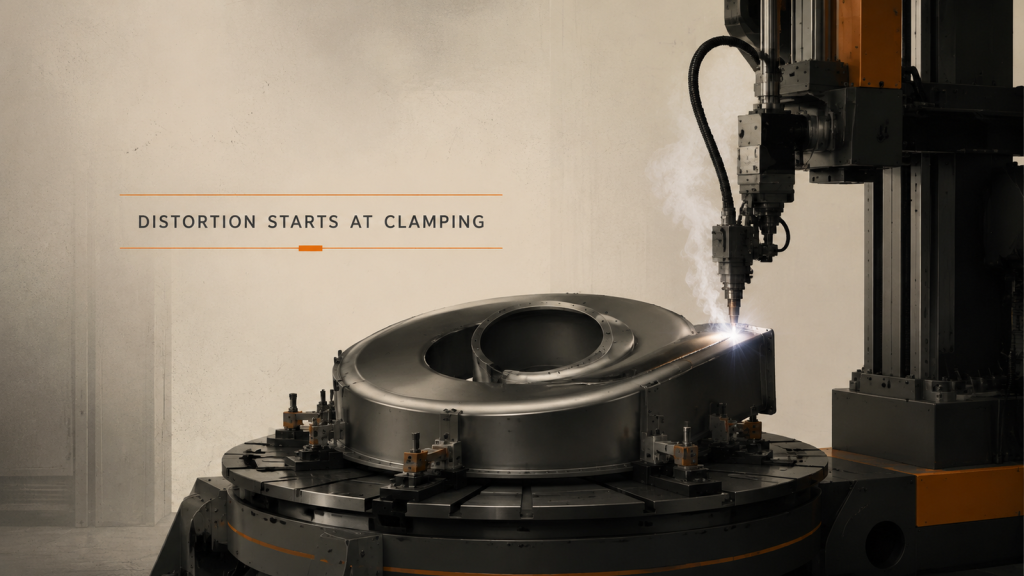
In thin-sheet welding, distortion causes more rework than weld defects. Clamp positions and weld sequence decide the final shape.