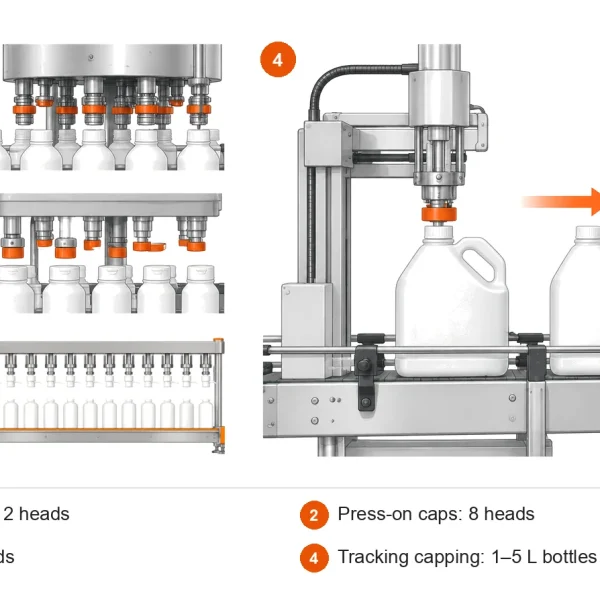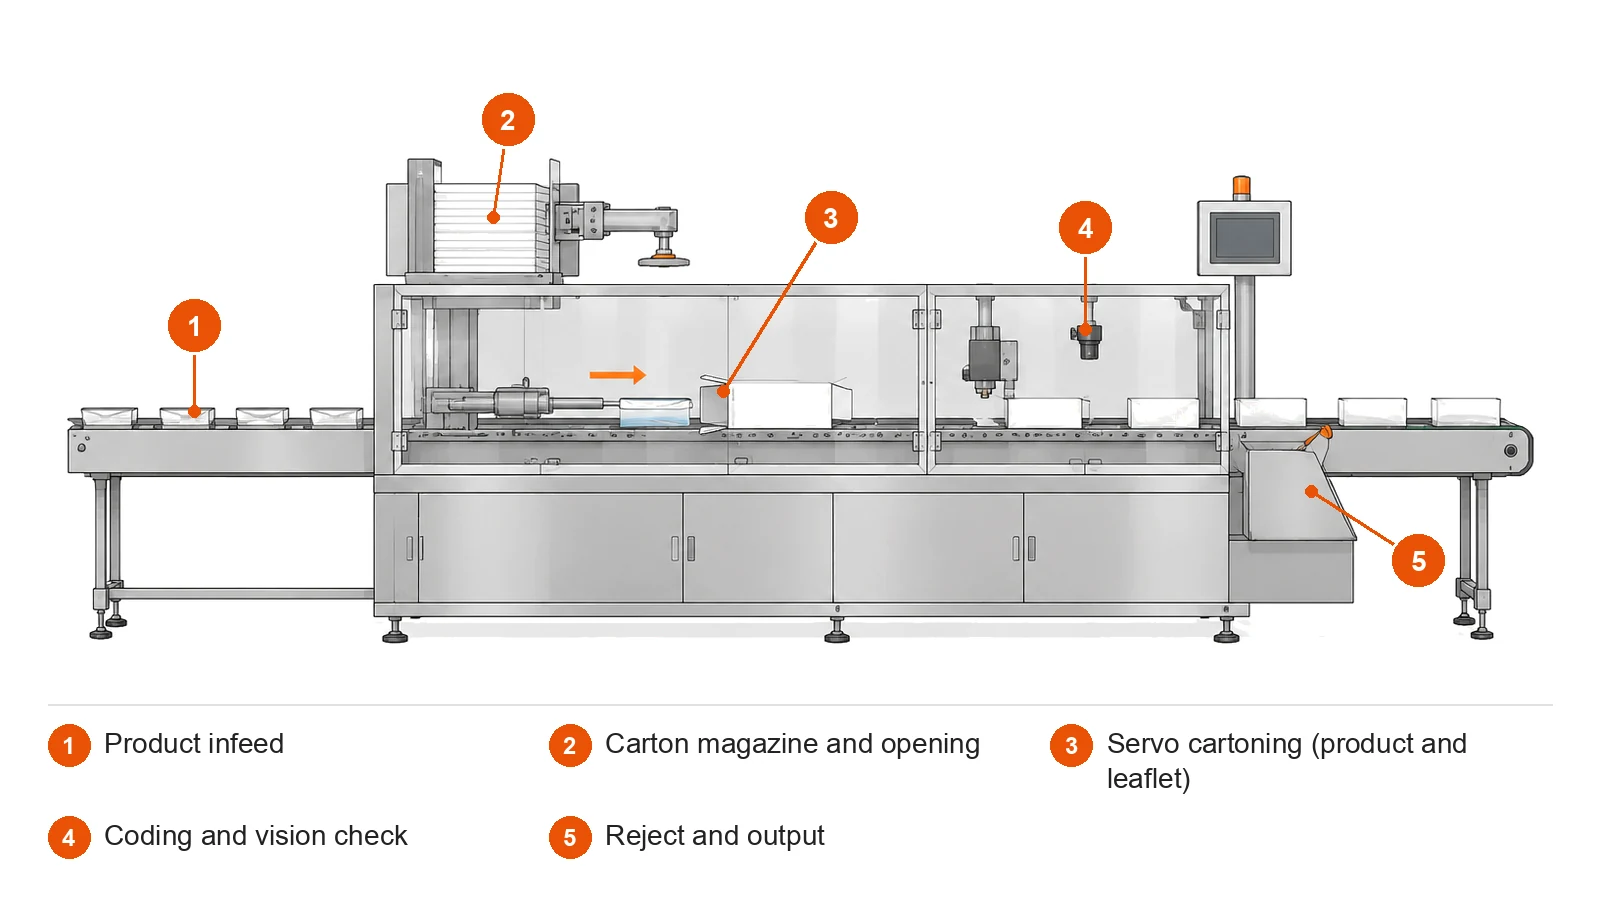
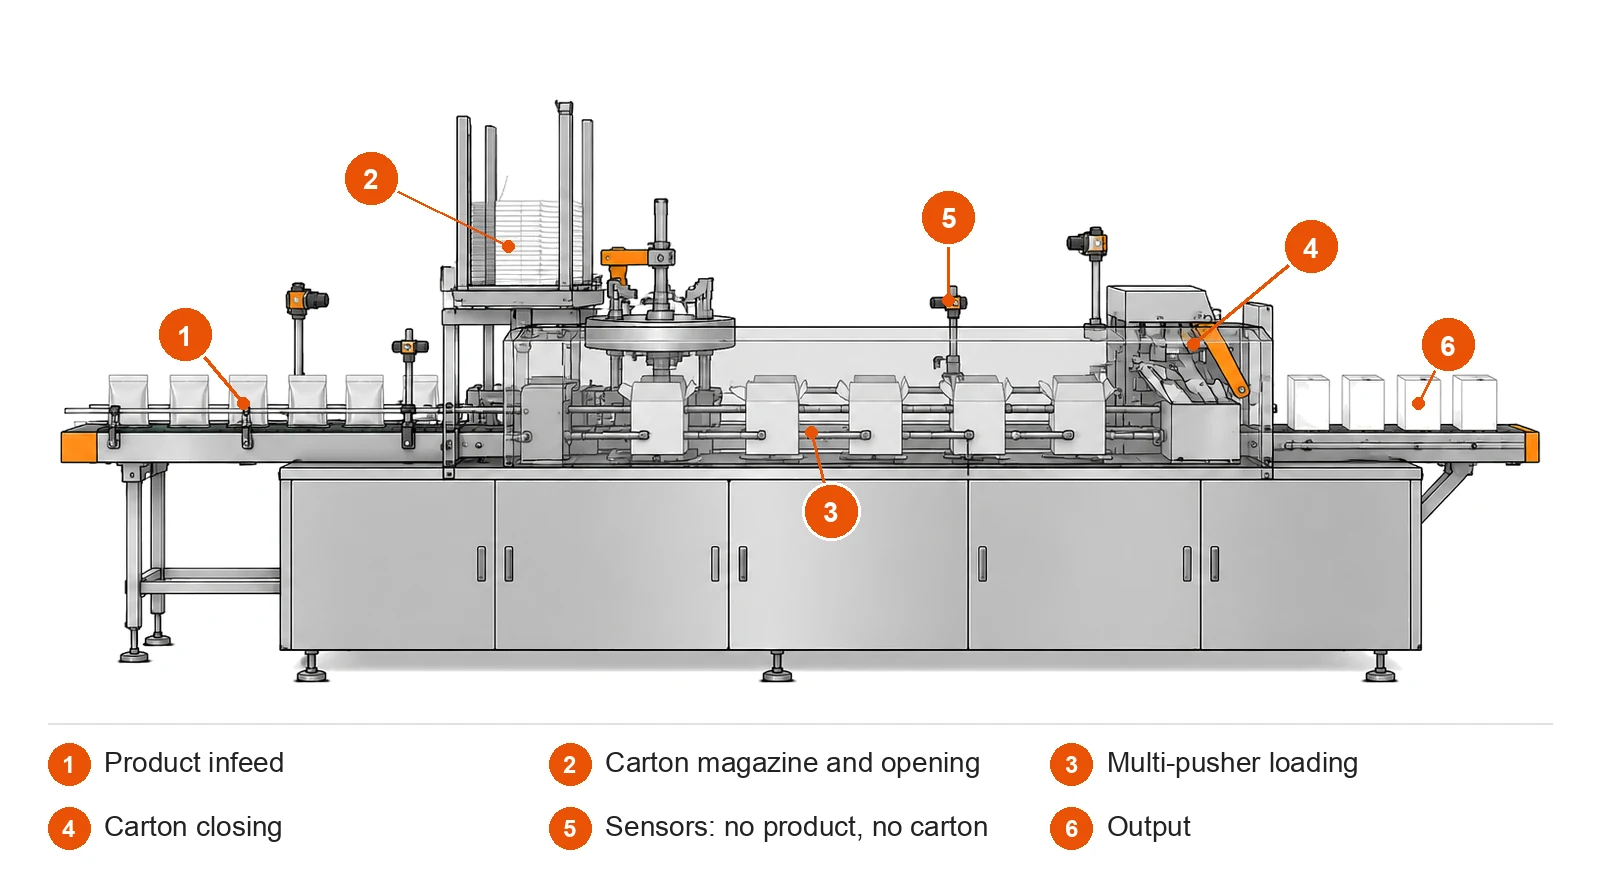
A horizontal cartoning machine is a cartoner in which the carton lies on its side while the product goes in. The machine opens a flat carton blank, the product is typically pushed in through the open end, and the end flaps are closed or glued. The exact process steps are configured for each product and project. This layout suits products that lie flat or are packed in blisters, sachets and pouches.
EVST builds the horizontal cartoner in two versions, both servo-controlled:
For how it compares with a vertical cartoner, see the カートニングマシン 概要。
| 断続的な、小容量カートンの範囲 | 断続的、大型カートン範囲 | 連続的な | |
|---|---|---|---|
| カートンサイズ(長さ×幅×高さ) | 70~160 × 25~100 × 16~40 mm | 60~220 × 25~120 × 20~70 mm | 100~220 × 25~120 × 25~65 mm |
| 速度 | 50カートン/分 | 50カートン/分 | 120カートン/分 |
| 運転と制御 | Servo system, simplified mechanism with fewer wear parts | Same as smaller-carton range | Servo main drive with overload protection; electronic cam, one-key speed setting on the HMI |
| 代表的な製品 | Contact lenses, dental implants, Class III medical devices | Same as smaller-carton range | Sachets, candy pouches, snack packs, personal-care gift sets, plug-in mosquito repellent kits |
速度はカートンのサイズによって異なります。
The intermittent cartoner is designed to sit in a line where every carton is identified and checked. It links directly with vision inspection and a 2D-code traceability system, and an industrial IoT platform monitors the process in real time. Its servo system and simplified mechanism cut the number of wear parts.
The continuous cartoner handles a wide range of carton sizes. Several pushers move product into the cartons without stopping, and an electronic cam links the motions so the operator changes speed with one key on the HMI instead of adjusting a frequency drive. The servo main drive has overload protection, protecting both the product and the machine.
Suitable product formats for the horizontal cartoner:
| 業種 | 製品 |
|---|---|
| 医療機器 | Contact lenses, dental implants in blisters, Class III device kits with leaflets |
| 医薬品とサプリメント | Herbal granule sachets, dietary fiber, collagen and vitamin C sachets |
| 食品および菓子類 | Candy pouches, snack packs, instant soup sachets |
| 家事と身の回りのケア | Foot-soak liquid sachets in gift boxes, baking soda sachets, plug-in mosquito repellent liquid with heater, personal-care gift sets |
Earlier implant lines were spread out over a large floor area; current layouts are built compactly, in the same way as the contact lens lines. For the full medical line, from parts presentation and leaflet insertion to UDI (Unique Device Identification) coding and inspection, see the 医療機器包装ライン.
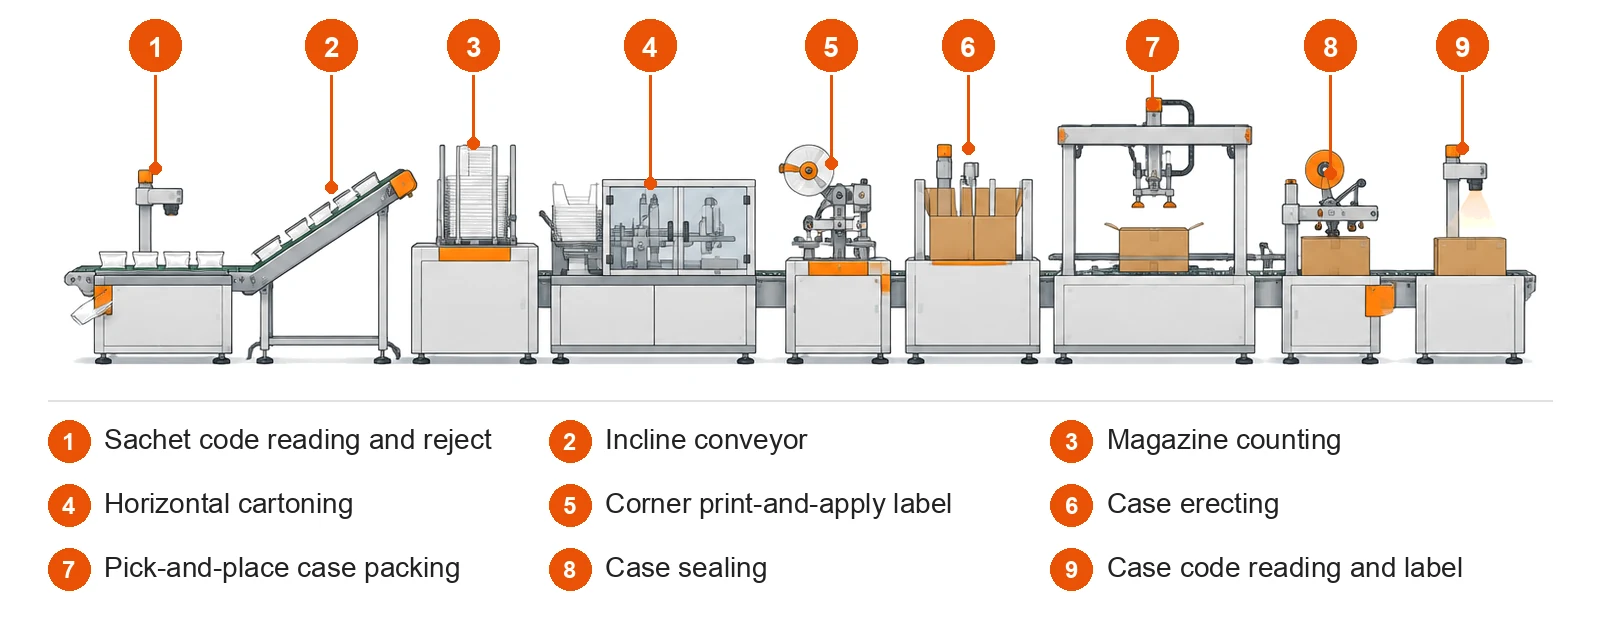
On sachet lines, each sachet’s code is read and failed sachets are rejected, the sachets climb an incline conveyor, a magazine counts them, and the horizontal cartoner loads each count into a carton. A corner label is printed and applied, and the cartons go on to case erecting, packing and sealing, with the case code read at the end.
| Item | 断続的な | 連続的な |
|---|---|---|
| カートンの長さ | 70–160 mm (smaller range) / 60–220 mm (larger range) | 100〜220 mm |
| カートンの幅 | 25–100 mm (smaller range) / 25–120 mm (larger range) | 25〜120 mm |
| カートンの高さ | 16–40 mm (smaller range) / 20–70 mm (larger range) | 25〜65 mm |
| 速度 | カートンサイズにもよるが、1分間に50カートン | カートンサイズにもよるが、1分間に120カートン |
| ステアリング位置 | サーボシステム | Servo main drive with overload protection; electronic cam |
| Controls and checks | Links to vision inspection and 2D-code traceability; industrial IoT platform for real-time process monitoring | One-key speed setting on the HMI, no frequency drive adjustment; multi-sensor detection: no product, no carton opened; no or missing carton, pause and alarm |
梱包箱と製品の構成は、プロジェクトごとに選択され、確認されます。
工場でのテスト時間は、テスト対象となるSKUの数が増えるにつれて長くなります。EVSTは、お客様のサンプルを確認後、プロジェクトごとに見積もりを提示いたします。
Products that lie flat or come in blisters, sachets or pouches: contact lenses, dental implants, medical device kits with leaflets, supplement and herbal granule sachets, candy pouches and snack packs. Upright bottles and tubes usually go on a 垂直カートン機.
EVST’s intermittent horizontal cartoner runs at 50 cartons per minute and the continuous version at 120 cartons per minute, both depending on carton size. On medical device lines with a camera at every step, the line speed is set by the checks rather than by the cartoner.
On contact lens lines, yes, for a power change: each blister is scanned and matched to its carton, so the line moves from one power to the next without stopping. A change of carton size is a format change, done within the machine’s carton size range; the formats tested before shipment are agreed for each project.
Yes. The intermittent cartoner links directly with vision inspection and a 2D-code traceability system, and on medical device lines the carton code is tied to the inner pouch and traceability card through the UDI system.
On a horizontal cartoner the end flaps are typically closed right after loading; the exact process steps are configured for each product and project. On medical device lines we have built, hot-melt glue sealing follows the cartoner where the carton requires it. The closing method is chosen with your carton design.
速度とカートンサイズは機械の仕様であり、カートンによって異なります。お客様の製品に適したカートナーは、プロジェクトごとに選定・確定されます。