
Run the same fixture with normal incoming parts before comparing weld times. A repeating hinge row is a candidate for robot welding when each joint lands in a predictable position and the order runs long enough to justify fixture setup and changeover. If an operator still has to bring individual hinge pieces into alignment by hand, keep those variants manual or improve their fit-up before committing to a robot.
Look for the joint after the clamp closes
The film shows a welding torch indexing along a long row of hinge pieces with repeated holes. An arc appears at successive positions along the worktable. The row makes the sequence easy to see. In a production trial, check the first and last joint after clamping: repeated holes can appear aligned while a contact edge or gap still varies.
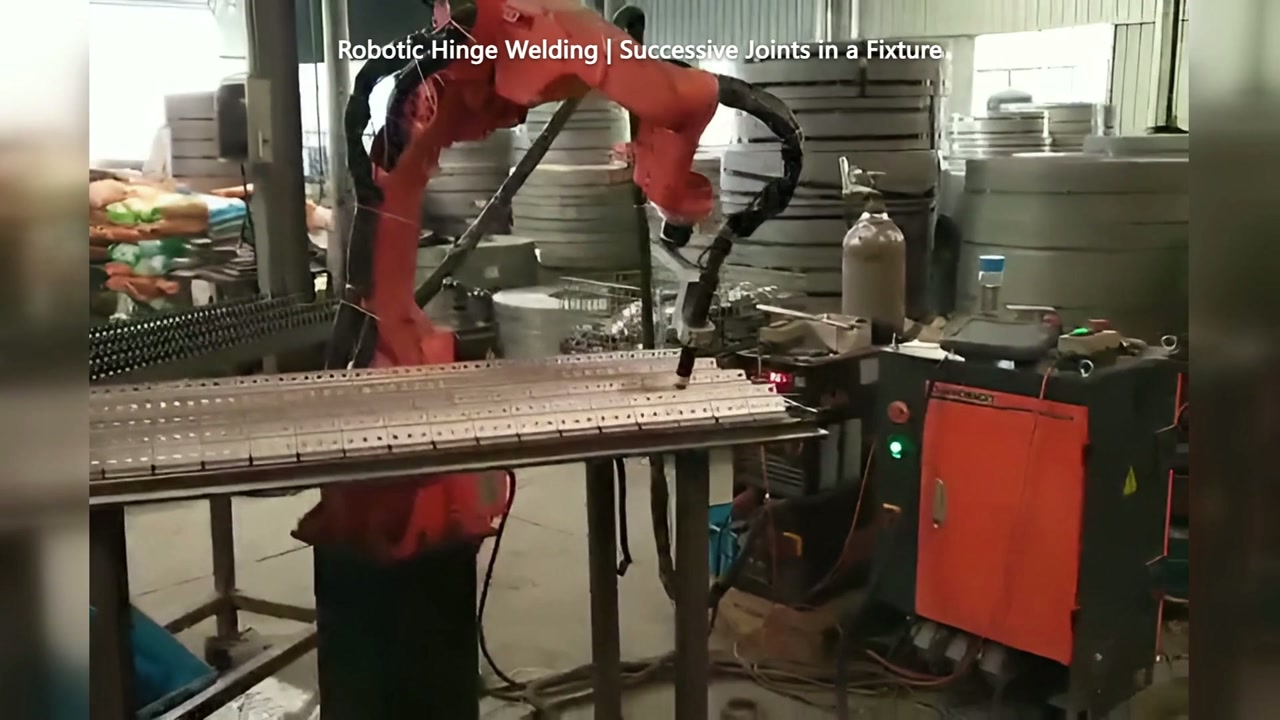
00:31 in the video. The torch is positioned above the hinge row toward the right side of the worktable.
Have the fixture locate the work using the surfaces that actually control the joint. Load pieces from normal production, close the fixture, then mark where the joint sits relative to the planned torch path. Check torch access with all the clamps closed. If a flange or clamp blocks one position, record that position separately; a trial with a single loose hinge will miss it.
Compare whole orders with the same acceptance check
| Tilauksen ehto | Käytännön seuraava askel |
|---|---|
| Long runs with repeatable joints in one fixture setting | Compare manual and robot times for a complete accepted row. Include loading, turning and unloading. |
| Short runs across hinge variants | Time the fixture change and first-piece approval on both routes. Keep orders manual where setup consumes the available run time. |
| One group repeats; another regularly needs hand adjustment | Trial the stable group on a robot and keep a manual path for the rest while upstream fit-up is improved. |
Use the same dimensional and weld acceptance criteria for both routes. An order with early fit-up corrections, end-of-row touch-up or frequent changeovers can take more work than its arc time suggests. Ask for an accepted row and its setup record, not only a timed weld demonstration.
If you have a hinge layout, a few representative variants and pictures of the gaps after loading, share them with EVST. We can discuss which families to include in a welding trial.